
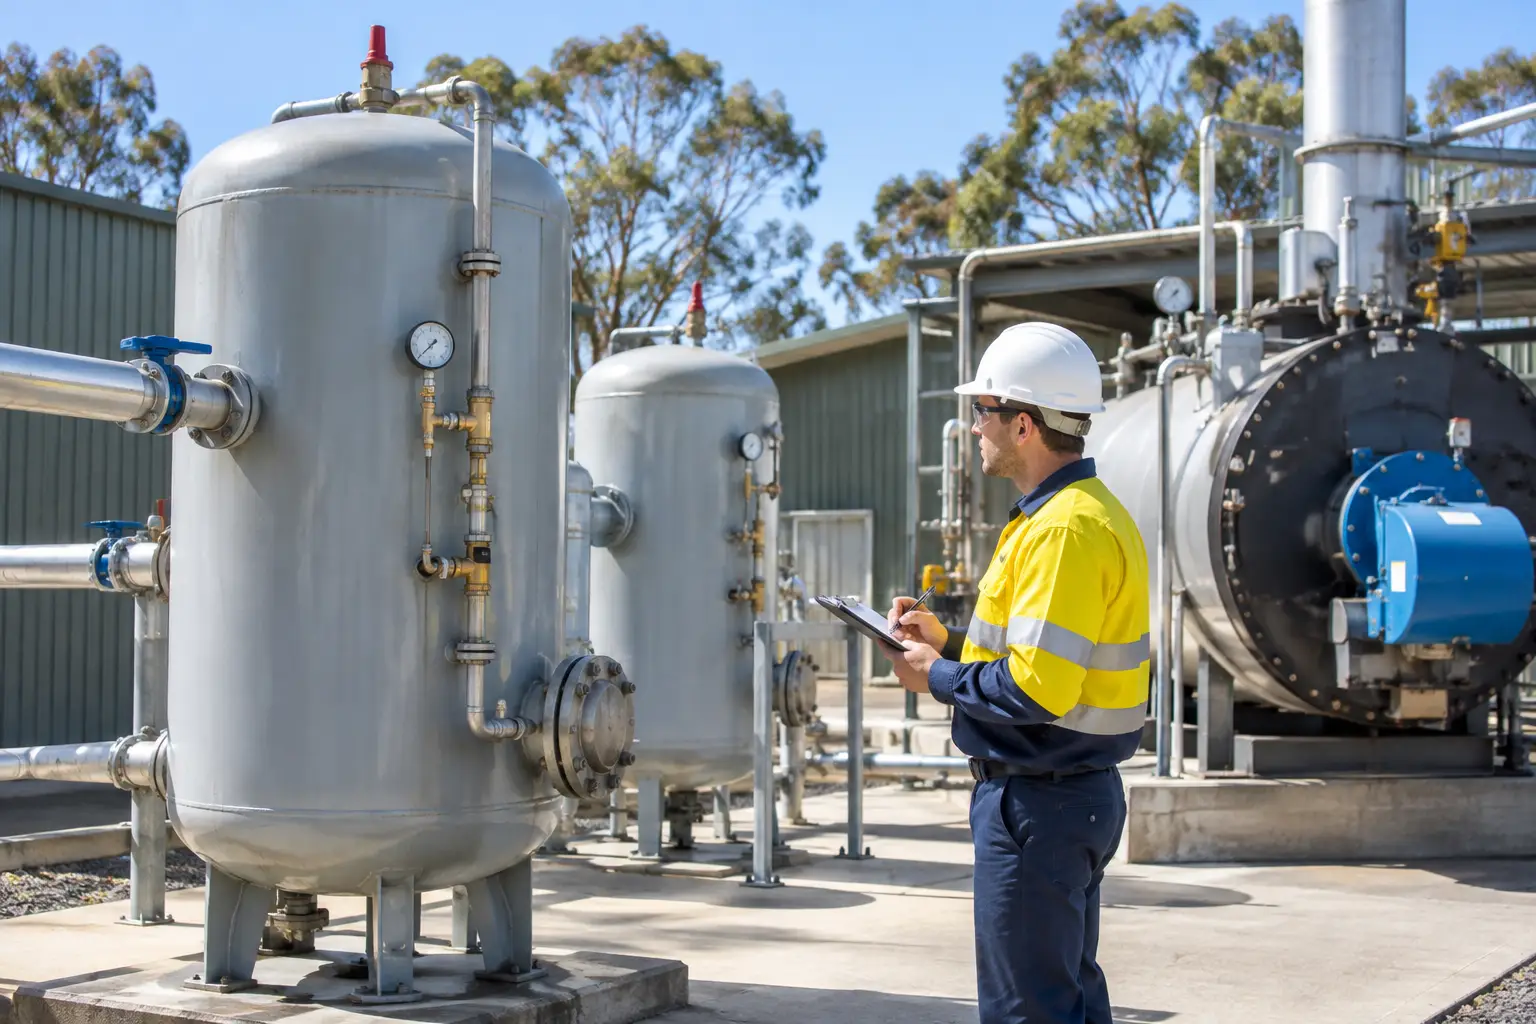
How to Manage Inspection Nonconformances at Plant
An inspection finding becomes a safety and operational issue only when it is left unclear, unowned or unverified. To manage inspection nonconformances effectively, pressure equipment owners need a controlled process that converts an identified condition into a documented decision, appropriate corrective action and objective evidence of close-out.
For boilers, pressure vessels and associated pressure equipment, this process must support the intent of AS 3788 while also recognising site-specific operating duty, degradation mechanisms, maintenance capability and regulatory obligations. A nonconformance is not simply a maintenance task. It is evidence that an asset, its records, its protective systems or its inspection status may not meet an applicable requirement.
What is an inspection nonconformance?
An inspection nonconformance is a condition identified during an in-service inspection, certification review or engineering assessment that does not satisfy the relevant requirement, acceptance criterion or documented basis for safe operation. It may concern the physical condition of equipment, an operating safeguard, inspection documentation or the management system supporting the asset.
Examples include active external corrosion, thinning beyond an allowable limit, damaged insulation concealing vessel condition, inoperative safety valves, missing identification, overdue internal inspections, incomplete repair records or an unresolved previous finding. The significance of each issue depends on the equipment’s design, service fluid, pressure and temperature, remaining wall thickness, consequence of failure and available safeguards.
A finding should not be downgraded merely because the equipment remains in production. Equally, not every departure requires an immediate shutdown. The proper response is determined by engineering evidence and risk, not production pressure or an arbitrary close-out period.
Manage inspection nonconformances through clear classification
The first decision is whether the nonconformance presents an immediate threat to safe operation. This requires the inspector’s observations to be considered alongside operating history, process conditions, design information and the function of the affected component.
Where a condition compromises pressure boundary integrity, overpressure protection or safe operation, the equipment may need to be removed from service, isolated or operated only under defined restrictions until an engineering assessment is completed. Examples can include significant localised corrosion, a suspected crack, failed pressure-relief protection or evidence of unapproved alteration.
Other findings may be managed through a planned corrective-action timeframe where the equipment remains demonstrably fit for continued service. A sound classification normally distinguishes between conditions requiring immediate action, priority action before the next planned operating period or shutdown, and lower-risk deficiencies requiring correction within an agreed timeframe.
Classification must be specific. A statement such as “repair as necessary” does not establish urgency, acceptance criteria or responsibility. The inspection report should identify the condition, relevant location, applicable requirement, required action and the basis for any continued-operation decision.
Separate the defect from its consequence
A damaged nameplate and a pressure boundary crack are both nonconformances, but they do not carry the same immediate consequence. Treating every finding as equally urgent can overwhelm maintenance systems and obscure the items that require prompt control.
Conversely, categorising a condition as administrative without examining its practical consequence can be unsafe. Missing inspection records may prevent verification of design pressure, material, repair history or inspection intervals. In some cases, the information gap itself warrants a conservative engineering response.
Establish ownership before the inspection is closed
An inspection report is not a corrective-action system. It provides the technical finding and, where appropriate, an independent recommendation. The asset owner must then assign responsibility for assessment, planning, repair, verification and record control.
Each nonconformance should have a nominated owner with authority to progress the action. For critical pressure equipment, this is often a maintenance manager, engineering manager or delegated responsible person. The action record should also identify the due date, risk controls while the item remains open and the evidence required for closure.
This distinction matters when work spans several parties. A maintenance contractor may complete the physical repair, but the owner remains responsible for ensuring the repair is suitable, documented and independently verified where required. Production personnel may manage temporary operating restrictions, while engineering determines whether those restrictions are technically acceptable.
A practical register should capture the equipment identifier, report reference, finding description, classification, responsible person, due date, interim controls, action status and closure evidence. It should be controlled as part of the site’s quality system, not maintained as an informal email trail.
Define corrective action, not just a repair request
Corrective action should address both the immediate condition and, where necessary, its cause. Replacing a corroded section without investigating why corrosion occurred may restore the asset temporarily but leave the degradation mechanism active.
For pressure equipment, the required action may involve repair, replacement, cleaning for further examination, non-destructive examination, thickness monitoring, a revised inspection interval, a fitness-for-service assessment or review of operating chemistry and process control. The appropriate pathway depends on the nature of the finding.
Repairs and alterations require particular discipline. The work scope should identify the applicable design and fabrication requirements, approved materials, welding procedures, welder qualifications, examination requirements, pressure testing where applicable and documentation to be retained. Repairs must not be treated as routine maintenance simply because they are carried out during a shutdown.
Where the original design standard, repair code or equipment history is uncertain, an engineering review should establish an appropriate basis before work begins. This may take longer than a straightforward replacement, but it avoids creating a new compliance problem while attempting to resolve an existing one.
Control equipment while action is pending
An open nonconformance needs active control. If continued operation is acceptable, the basis for that decision should be documented, including any limits on pressure, temperature, duty cycle, service fluid or inspection frequency.
Interim controls can include reducing operating pressure, increasing operator checks, conducting additional thickness measurements, isolating a redundant item, limiting service until the next shutdown or applying a defined monitoring plan. These controls are not a substitute for corrective action. They are temporary measures to manage risk while the permanent action is completed.
The decision should be reviewed if process conditions change. An interim arrangement developed for intermittent, low-temperature service may no longer be valid after a production increase, a process change or a change in fluid composition.
Verify close-out with objective evidence
A nonconformance is not closed because a work order shows “complete”. Closure requires evidence that the action has met the defined requirement and that the equipment is suitable for its intended service.
For a simple administrative issue, evidence may be a recovered document or corrected asset record. For a physical defect, close-out may require photographs, material certificates, weld records, non-destructive examination reports, pressure-test records, thickness readings or a post-repair inspection. The level of verification should reflect the safety significance of the original finding.
Independent verification is particularly valuable where the repair affects a pressure boundary, pressure-relief device, design condition or certification status. An AICIP-accredited in-service inspector can assess whether the inspection findings, repair evidence and condition of the equipment support return to service under the applicable inspection framework.
Pressure Vessel Inspections Pty Ltd provides independent inspection and engineering advice without manufacturer, repairer or asset-owner bias. That separation helps ensure close-out decisions are based on equipment integrity and compliance evidence rather than the commercial interest of the party undertaking the work.
Maintain records that stand up to review
Defensible records allow a site to show what was found, how it was assessed, what was done and who verified the result. They also give future inspectors and engineers the information needed to identify recurring damage, assess remaining life and set appropriate inspection intervals.
Retain the original inspection report, nonconformance record, risk assessment where used, approved repair scope, contractor documentation, test and examination results, engineering calculations or assessments, close-out approval and any updated equipment history. Asset registers should be updated promptly where the repair changes equipment details, inspection requirements or operating limits.
Under an ISO 9001:2015-aligned quality approach, the objective is traceability rather than paperwork for its own sake. A complete record supports consistent decisions across personnel changes, insurance reviews, regulator enquiries and future outage planning.
Use trends to prevent repeat findings
A single nonconformance should be resolved properly. Repeated nonconformances should trigger a wider review. Recurring corrosion under insulation, repeated overdue safety-valve servicing or persistent gaps in repair records can indicate a weakness in maintenance planning, process control, inspection access or document management.
Trend review is most useful when findings are grouped by equipment type, damage mechanism, location, service and root cause. This can identify where condition-based monitoring, modified insulation practice, revised operating controls or a changed inspection strategy will deliver better risk reduction than repeated reactive repairs.
The most useful nonconformance process is one that gives plant personnel a clear next action while preserving independent technical judgement. When a finding is recorded precisely, assessed against the right criteria, controlled while open and closed with evidence, it becomes a practical safeguard for people, production and the long-term integrity of pressure equipment.


Comments